How to Choose a Reliable Chrome Electroplating Supplier?

Choosing a reliable chrome electroplating supplier requires more than comparing surface brightness or unit prices. A mirror-like finish can hide weak adhesion, uneven thickness, or poor corrosion resistance. The real test begins beneath the shine.

George DiBari, a respected electroplating engineer and author, states, “The quality of the finished product is determined by the quality of the preparation.” This principle remains highly relevant. A dependable supplier should explain how it cleans, activates, polishes, and prepares each substrate before plating. Ask whether the process suits steel, aluminum, brass, zinc, or engineered plastics. Different materials demand different pretreatment methods.

Look closely at the facility. Are operators checking bath temperature, chemical concentration, current density, and plating time? Are thickness readings recorded across edges, corners, and recessed areas? These small details reveal process discipline. Request sample parts, adhesion results, corrosion-testing data, and inspection records. A serious supplier will discuss failures honestly, not only display perfect samples.

Experience matters here.

Reliable communication matters too. The supplier should confirm tolerances, cosmetic expectations, packaging requirements, and delivery risks in writing. Certifications can support confidence, but they should not replace technical evidence. A certificate alone cannot repair a poorly prepared surface.

There is also room for reflection. The cheapest quotation may become expensive after peeling, discoloration, rework, or rejected assemblies. However, not every premium-priced supplier is automatically better. Compare measurable controls, documented results, and practical responsiveness. The best chrome electroplating partner makes quality visible before production begins.
How to Choose a Reliable Chrome Electroplating Supplier?

Define Your Chrome Plating Requirements and Quality Standards

How to Choose a Reliable Chrome Electroplating Supplier?

Define Your Chrome Plating Requirements and Quality Standards

When choosing a reliable chrome electroplating supplier, start with a written definition of your plating requirements. Do not describe the finish as simply “shiny chrome.” Specify the base material, part dimensions, plating area, coating thickness, surface texture, and required appearance. State whether the part needs decorative brightness, wear resistance, hardness, or corrosion protection.

Operating conditions matter. Humidity, salt exposure, temperature changes, and repeated contact can affect the correct process. Some specifications are easy to miss, especially on edges, holes, and masked areas.

Quality standards should be measurable, not based only on supplier photographs. Ask for agreed limits on thickness, adhesion, porosity, roughness, color, and visible defects. Include inspection methods and sampling frequency in the purchase documents.

For critical components, request test records, calibration details, and batch traceability. A capable supplier should explain how cleaning, polishing, activation, and plating are controlled.

I have seen attractive samples fail after poor preparation. Surface preparation is not a minor step.

Ask for a sample part or trial run before approving volume production. Compare the results with your drawings and actual service conditions.

If a supplier promises perfect results without asking technical questions, pause. That confidence may be convenient, but it is not evidence.

Request corrective-action records when defects occur, and check whether the response identifies the real cause. Independent inspection can also be useful.

Still, no checklist replaces clear communication. Leave room for review. Your requirements may change after the first parts face real wear.

Verify the Supplier’s Technical Expertise and Production Capabilities

How to Choose a Reliable Chrome Electroplating Supplier?

Verify the Supplier’s Technical Expertise and Production Capabilities

A reliable chrome electroplating supplier should explain its process, not merely display shiny samples. Ask who controls cleaning, activation, plating, rinsing, and final inspection. Experienced engineers can discuss bath chemistry, current density, temperature, and cycle time in practical terms. They should explain how part geometry affects coating coverage. Deep recesses and sharp edges often plate differently. That detail matters. Request process documents, training records, and examples of corrective actions. A confident supplier will share evidence without hiding behind vague claims.

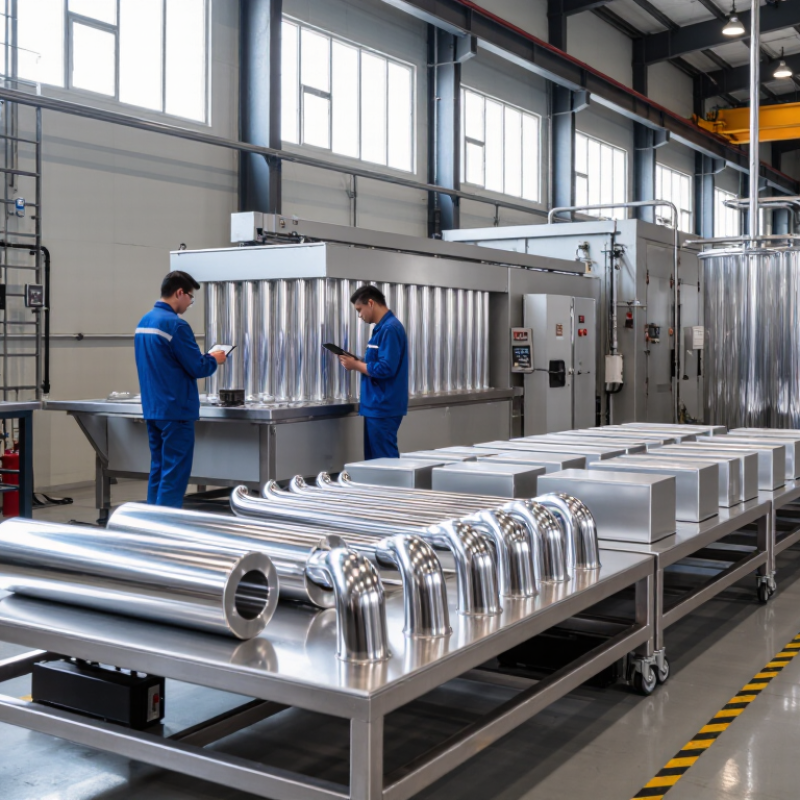
Production capability must be visible on the factory floor. Check whether separate lines support different substrates and part sizes. Inspect rectifiers, filtration systems, drying equipment, and thickness gauges. Ask how operators record bath conditions during each shift. Reliable records should connect a batch to its operator, line, date, and inspection results. Review test methods for adhesion, coating thickness, appearance, and corrosion resistance. A cross-section report can reveal uneven layers that a bright surface conceals. Small details matter more than impressive machinery.

Request a pilot lot before approving regular production. Compare its dimensions, gloss, color consistency, and defect rate with your drawings. Ask what happens when results fall outside the agreed range. Good suppliers isolate affected parts, investigate root causes, and document the response. No supplier is perfect. Their response to mistakes is more revealing than a flawless sample. Factory visits can also mislead if only selected areas are shown. Bring a short checklist, ask unexpected questions, and verify capacity during a normal production shift.

How to Choose a Reliable Chrome Electroplating Supplier? - Verify the Supplier’s Technical Expertise and Production Capabilities

Verification Dimension What to Verify Reference Benchmark or Technical Expectation Recommended Evidence Priority
Process Knowledge Ability to distinguish decorative chrome plating from hard chrome plating and select a suitable process sequence. The supplier should explain the roles of cleaning, activation, nickel or intermediate layers, chrome deposition, rinsing, drying, and inspection. Written process flow, technical review records, sample process specifications, and answers to application-specific questions. High
Plating Thickness Control Capability to control coating thickness according to the drawing, functional requirement, and tolerance. Thickness should be measured at defined locations using calibrated instruments; local thickness limits should be stated rather than relying only on an average value. Thickness reports, measurement-point diagrams, calibration certificates, and sample inspection records. High
Surface Preparation Control of degreasing, alkaline cleaning, acid activation, masking, and pre-treatment before plating. The process should prevent oil, oxide, scale, and handling contamination from reducing adhesion or creating pits, blisters, and bare areas. Pre-treatment parameters, bath-maintenance logs, surface-cleanliness checks, and defect-prevention procedures. High
Adhesion Performance Verification that the plated layer is firmly bonded to the substrate and intermediate layers. The supplier should use a suitable adhesion test method for the substrate and coating system, with acceptance criteria agreed before production. Adhesion test reports, test-method references, failure photographs when applicable, and corrective-action records. High
Corrosion Testing Ability to evaluate corrosion resistance for the intended environment and service life. Neutral salt spray testing should be performed according to ISO 9227 or ASTM B117 when specified; test duration and acceptance criteria must match the product requirement. Independent or in-house corrosion-test reports, chamber maintenance records, exposure duration, and rating criteria. High
Hardness and Wear Resistance Capability to verify hardness and wear resistance for functional hard-chrome applications. The supplier should define the hardness method, load, surface condition, coating thickness, and wear-test procedure instead of quoting hardness without test conditions. Hardness reports, wear-test data, equipment details, and application-specific qualification results. Medium
Dimensional Capability Ability to compensate for coating build-up and maintain final dimensions on precision components. Plating allowance, masking areas, edge effects, grinding or polishing requirements, and final dimensional tolerances should be documented before production. Approved drawings, process allowances, coordinate or gauge inspection reports, and first-article inspection results. High
Production Equipment Availability and suitability of rectifiers, plating tanks, filtration, heating or cooling, agitation, rinsing, and wastewater-treatment systems. Equipment capacity should match the part size, load weight, current demand, bath chemistry, and required production volume. Equipment list, rated capacities, preventive-maintenance records, tank-control records, and production-line photographs. High
Electrical Process Control Control of current density, voltage, plating time, contact quality, and part positioning. The supplier should record key electrical parameters for each batch and use stable fixturing to reduce uneven thickness and burn defects. Batch records, rectifier data, fixture drawings, current-density calculations, and process-monitoring logs. High
Bath Chemistry Management Routine control of metal concentration, additives, contaminants, temperature, pH where applicable, and solution condition. Bath analysis frequency and control limits should be defined; corrective additions should be traceable and approved by qualified personnel. Laboratory analysis reports, chemical-addition logs, bath history, control charts, and supplier chemical certificates. High
Inspection Equipment Availability of suitable instruments for coating thickness, appearance, dimensions, roughness, adhesion, and corrosion evaluation. Inspection equipment should be appropriate for the substrate and coating system, regularly calibrated, and supported by documented measurement procedures. Instrument register, calibration certificates, measurement-system procedures, and operator training records. High
Quality Management Effectiveness of the supplier’s quality system, nonconformance control, traceability, and corrective-action process. An ISO 9001-certified quality management system is a useful indicator, but process records and actual corrective-action performance should also be reviewed. Valid certificate from an accredited certification body, internal audit records, nonconformance reports, and corrective-action examples. High
Production Capacity Ability to meet required batch size, monthly volume, lead time, and peak-demand requirements. Capacity should be demonstrated using realistic part-loading assumptions, available shifts, equipment utilization, inspection time, and planned maintenance. Capacity calculation, production schedule, bottleneck analysis, staffing plan, and anonymized delivery-performance data. High
Pilot Production Willingness to perform sample plating or a first-article run before mass production. The pilot should confirm appearance, thickness distribution, adhesion, dimensions, corrosion performance, packaging, and repeatability. Approved samples, first-article report, capability results, defect analysis, and signed acceptance criteria. High
Traceability Ability to link raw material, production batch, chemical condition, operators, inspection results, and shipment records. Each production lot should have a unique identifier and retrievable records covering processing and final inspection. Anonymized batch traveler, lot labels, inspection reports, retention policy, and sample retrieval demonstration. High
Environmental and Safety Controls Management of chromium-containing chemicals, wastewater, worker protection, ventilation, and regulatory obligations. The supplier should provide documented chemical-handling procedures, wastewater controls, employee training, and legally required environmental permits. Relevant permits, wastewater-test records, safety data sheets, training records, emergency procedures, and audit results. High
Technical Communication Quality and speed of responses to drawings, tolerances, test requirements, defects, and engineering changes. A reliable supplier should identify technical risks before production and provide clear, measurable recommendations rather than accepting every requirement without review. Technical review form, issue-resolution history, engineering-change records, and response-time performance. Medium
Total Evaluation Overall decision based on technical competence, repeatability, capacity, compliance, and verifiable records. Select a supplier only after document review, sample approval, capability confirmation, and successful verification of critical coating properties. Completed supplier audit checklist, approved sample, signed quality agreement, and documented risk assessment. High

Assess Plating Processes, Materials, and Environmental Compliance

Choosing a reliable chrome electroplating supplier requires more than inspecting a bright sample. The surface should reflect a controlled process, not temporary polish. Ask how parts are cleaned, activated, plated, rinsed, and dried. Each stage affects adhesion and corrosion resistance. Request records showing coating thickness, bath temperature, current density, and inspection frequency. A supplier should explain these details clearly.

Materials also deserve close attention. Confirm the base metal, pretreatment chemicals, copper or nickel layers, and final chrome layer. Traceable material certificates reduce uncertainty between batches. Practical testing may include thickness measurement, adhesion checks, salt spray exposure, and visual inspection under consistent lighting. Small defects matter. Blisters, cloudy areas, pinholes, or uneven edges often reveal weak process control. A perfect sample can still mislead if production consistency is unproven.

Environmental compliance should be reviewed with the same care. Ask for current permits, wastewater treatment records, air-emission controls, chemical storage procedures, and waste-disposal documentation. The supplier should identify how hazardous residues are collected and monitored. Independent laboratory reports can support, but not replace, an on-site assessment. During a review, look for labeled containers, sealed drainage areas, functioning ventilation, and clear emergency instructions. Some suppliers present excellent paperwork but weak factory habits. That gap deserves attention. I would also record unanswered questions, because uncertainty is part of the purchasing risk.

Review Quality Control Systems, Certifications, and Testing Methods

How to Choose a Reliable Chrome Electroplating Supplier?

A reliable chrome electroplating supplier should show more than a bright sample. Ask to review its quality control system, process records, and inspection responsibilities. ISO 9001 certification is useful, but it does not guarantee perfect plating. The ISO Survey 2022 reported more than 1.2 million ISO 9001 certificates worldwide. That number shows broad adoption, not automatic competence. Verify the certificate’s scope, validity, issuing body, and included processes. A supplier should also control bath chemistry, temperature, current density, cleaning, and rinse quality. These details often decide whether a coating survives real service.

Request measurable test results, not general promises. Thickness can be checked through X-ray fluorescence or metallographic cross-sections. Adhesion testing should follow a recognized ASTM or ISO method. Porosity testing matters when the coating protects steel or supports corrosion resistance. Salt-spray testing, such as ASTM B117, can compare batches, but it cannot perfectly predict field life. The NACE IMPACT study estimated global corrosion costs at 2.5 trillion dollars, or 3.4 percent of global GDP. Better prevention deserves serious attention.

Look for calibrated instruments, traceable reference samples, and retained inspection records. Ask how rejected parts are isolated and how corrective actions are verified. A serious supplier can explain sampling plans and provide certificates of analysis for incoming materials. Visit the plant if possible. Observe rack contact points, bath cleanliness, ventilation, and operator discipline. One uncomfortable truth remains: audits capture a moment. Even a well-documented system can drift, so periodic independent testing and production-site reviews are still worthwhile.

Compare Pricing, Lead Times, Communication, and After-Sales Support

How to Choose a Reliable Chrome Electroplating Supplier?

A reliable supplier should make pricing easy to inspect, not merely attractive. Request separate costs for tooling, preparation, plating, inspection, packaging, and freight. Ask whether the quote includes thickness testing and rework. A low unit price can hide setup fees or inconsistent surface preparation. Compare at least three quotations using the same drawing and finish requirements. I once accepted a cheaper quote without checking masking details. The final parts needed extra polishing. That mistake changed my evaluation method.

Lead time should be written as production days, not vague promises. Confirm sample timing, capacity during peak periods, and approval deadlines. Ask what happens if incoming parts arrive late or fail inspection. A practical supplier shares a process schedule with checkpoints. Communication matters just as much. During a trial order, note response speed, technical clarity, and willingness to document changes. Fast replies are not enough. Precise replies matter more.

After-sales support becomes visible when something goes wrong. Confirm the warranty scope, claim procedure, evidence requirements, and response target before ordering. Ask for inspection records, corrective-action reports, and replacement terms. A dependable supplier should discuss possible defects without becoming defensive. Request a small pilot batch before committing to volume. Review gloss, adhesion, dimensions, and packaging after delivery. I still find supplier comparisons imperfect because production problems can appear later. Keep written records and review performance across several orders, not one successful shipment.